Hey there, if you’ve ever been deep in the process of designing a distillation, absorption, or extraction system, you’ve definitely bumped into the term “column efficiency” when talking about packed columns. As a packed column supplier, I get it—this stuff can feel super jargon-heavy, like decoding a weird lab recipe that no one wrote down clearly. Most folks just know it matters, but they don’t always have a straightforward breakdown of what it actually is, why it’s a big deal, and how to nail it for your project. Let’s keep this real, no stuffy textbook fluff, just the straight talk you need if you’re specs-ing a new packed column or troubleshooting an old one. Packed Column

First off, let’s kill the confusion: column efficiency isn’t some random “how well it works” buzzword. It’s a measure of how good your packed column is at separating two or more components of a liquid (or gas) mixture. Think of it like grading a coffee filter: a bad filter lets all the coffee grounds slip through, so your brew is gritty (messy separation), while a great one traps almost all the grounds, giving you a smooth cup (clean split of your mixture). Packed columns do this separation through mass transfer—when gas and liquid flow past each other, they swap components to pull them apart. The more complete that swap, the higher the efficiency.
But here’s the catch: it’s never perfect. Even the best packed columns have some loss, that’s why efficiency is always a number between zero and something less than ideal. We usually call the ideal limit a “theoretical plate” (or theoretical stage)—that’s a hypothetical section where gas and liquid mix perfectly, reach equilibrium, and are split into separate streams that are as pure as possible. Actual packed columns don’t hit that perfect equilibrium, so we use “HETP” (height equivalent to a theoretical plate) to make this easy. HETP is basically how tall your packed bed needs to be to equal one of those ideal theoretical plates. Lower HETP = way better efficiency, because you need less packing to get the same separation. That’s the sweet spot everyone chases.
Now, let’s talk about the two main types of efficiency you’ll hear about—don’t zone out, these are actually useful for picking the right packing. There’s overall column efficiency (E₀), which is the big-picture number that compares all the actual plates in your column to theoretical ones. Then there’s point efficiency (E₀G or E₀L, depending if you’re tracking gas or liquid), which is the efficiency of a tiny, single section of packing. Most of the time when someone asks, they mean overall efficiency, so that’s what we’ll focus on here.
Wait, let’s ground this in a real example, since numbers help. Say you’re separating ethanol and water for a small beverage plant. You calculate you need 10 theoretical plates to get the alcohol content just right. If your overall column efficiency is 70%, that means you only need 10 divided by 0.7 = ~14 actual plates. If your efficiency drops to 50%, you need 20 actual plates. That’s a huge difference in column size, cost, and space—so yeah, efficiency isn’t trivial.
Now, what actually affects column efficiency? This is where things get actionable, not just theoretical. I’ve seen projects go wrong because they ignored these factors, so take notes.
First up, packing type and size. This is the biggest lever you can pull, in my experience. Random packing (the little ceramic or metal rings, saddles, or spheres you dump into the column) versus structured packing (those corrugated metal or plastic sheets stacked in a precise pattern) make a massive difference. Structured packing usually has way higher efficiency—lower HETP—for the same flow rate, but it’s also more expensive up front. Random packing is cheaper, easier to install, but needs to be sized right. If your packing is too big, there’s gaps between pieces, so gas and liquid shortcut past each other (that’s called channeling, ugh, the worst enemy of efficiency). If it’s too small, you get too much pressure drop, which wastes energy moving gas through the column. I always tell customers: match packing size to your column diameter. Rule of thumb, the packing size should be 1/10 to 1/20 of the column diameter, that avoids channeling.
Next, flow rates of gas and liquid. This is called the “operating window” of the column. If you go too slow, liquid doesn’t spread evenly over the packing, so you get that channeling I just mentioned—efficiency tanks. If you go too fast, two bad things happen: either flooding (gas pressure gets so high it pushes liquid back up the column, making separation impossible) or loading (liquid starts pooling on the packing, so gas can’t flow properly, efficiency drops sharply). Most good packed columns have a sweet spot between minimum flow (where channeling starts) and flood flow—stay in that, and efficiency stays consistent. I see so many operators push their column too hard to get more output, and they kill efficiency in the process. It’s a tradeoff, not a win.
Then there’s liquid distribution. Even if you pick the best packing and right flow rates, if your liquid is dumped unevenly at the top of the column, half the packing gets no liquid, so separation is garbage. We call this “maldistribution,” and it’s a silent killer of efficiency that’s hard to fix once the column is built. Early in a project, we recommend liquid distributors (those perforated plates or spray nozzles at the top) that spread liquid evenly, and sometimes re-distributors every few feet down the column to fix any maldistribution that creeps in as liquid flows. I once worked with a small distillery that had a column that barely worked, turned out their cheap plastic distributor only had 10 holes for a 3ft wide column—total maldistribution, they were shocked how much just swapping the distributor fixed their separation.
Fluid properties matter too. If you’re working with super viscous liquids (like heavy oils or polymers), the liquid moves slower through the packing, so mass transfer is worse—efficiency drops. Viscosity is a big one for these systems. Surfactants, pH, even temperature can change how gas and liquid interact at the packing surface, so that tweaks efficiency too. For example, if you’re separating a mixture that foams a lot, you have to adjust flow rates way below flood, because foaming causes entrainment (gas carrying liquid up the column) which messes up separation.
Now, let’s get to how you actually calculate this, because “I know it when I see it” doesn’t cut it for engineering. The main number we use for packed columns is HETP, like I mentioned earlier. HETP is usually determined experimentally for specific packing and flow conditions, but there are also correlations (like the Sherwood number or Gilliland correlation) that engineers use to estimate HETP during design. For structured packing, HETP is often pretty consistent across a range of flow rates, which is why it’s so popular for high-throughput operations like refineries. For random packing, HETP can vary more, especially near the flood point.
Overall column efficiency (E₀) is calculated by dividing the number of theoretical plates (Nₜ) by the actual number of separation stages (Nₐ) in the column, times 100 to get a percentage. So E₀ = (Nₜ / Nₐ) * 100. For most industrial packed columns, E₀ ranges from 50% to 90%—anything above 90% is super rare, only for very clean, low-viscosity mixtures. Below 50% usually means you messed up the packing size, distribution, or flow rates.
Wait, let’s bust a myth here: higher efficiency isn’t always better. If you only care about rough separation, a cheaper, lower-efficiency random packing might be all you need. But if you need ultra-pure product (like for pharma or fine chemicals), higher efficiency structured packing is worth the extra cost, because you need fewer theoretical plates. It’s a balance between capital cost (the column, packing, installation) and operating cost (energy to run the column, maintenance). As a supplier, I don’t push the most expensive packing on every customer—I listen to what they need, their budget, their production goals, and recommend what gives the best total value.
I also get a lot of questions from people who have an old column that’s not performing as well as it used to. Why does packed column efficiency drop over time? Common reasons: packing fouling (build-up of solids, gunk, or scale on the packing surface, which blocks mass transfer), damaged packing (pieces breaking, shifting, leading to channeling), or worn distributors (holes getting clogged, nozzles breaking, maldistribution coming back). A quick check: pull a sample of your packed bed, check for clogs, test the liquid distribution at the top, and measure HETP. Usually fixing one of those issues brings efficiency back up, no need for a whole new column.
So, wrapping this up: column efficiency is all about how well your packed column separates mixture components, measured by HETP and overall efficiency. It depends on packing type/size, flow rates, fluid properties, and distribution. Get these right, and you get a column that works like it’s supposed to, saves energy, and gives you the product quality you need.
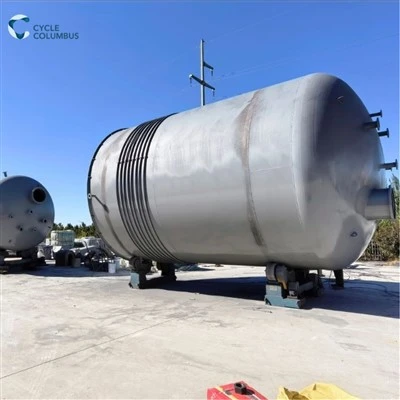
If you’re in the middle of a project, struggling with a underperforming column, or just want to spec the right packed column for your next job, don’t overcomplicate it. We’ve worked with everything from small craft distilleries to big refineries, and we can help you nail the efficiency for your specific mixture, flow rate, and budget. Reach out for a chat, no pressure, just straight answers tailored to your needs.
Ozone Generation References:
- Perry, J. H. (Ed.). (1997). Perry’s Chemical Engineers’ Handbook (7th ed.). McGraw-Hill.
- McCabe, W. L., Smith, J. C., & Harriott, P. (2005). Unit Operations of Chemical Engineering (7th ed.). McGraw-Hill.
- Strigle, R. F. (1994). Packed Tower Design and Applications (2nd ed.). Gulf Professional Publishing.
- Eckert, J. S. (1975). “Selection of Packings for Distillation.” Chemical Engineering Progress, 71(5), 54–61.
Beijing Cycle Columbus Environmental Science & Technology Co., Ltd.
Beijing Cycle Columbus Environmental Science & Technology Co., Ltd. is one of the most professional packed column manufacturers and suppliers in China. We are committed to providing high quality customized products with competitive price. Please feel free to buy advanced packed column made in China here from our factory. Also, quotation is available.
Address: 1201, 12/F, Tower B, Bldg 8, Guancheng Garden, Haidian District, Beijing, China
E-mail: Info@saikekanglun.com
WebSite: https://www.cycle-columbus.com/
